COVO KNOWLEDGE
Spring-Loaded Hemming Die: Pre-Bend and Flatten in Two Strokes
Published:
Updated:
See how a spring-loaded hemming die makes a 30° pre-bend and closes a hem in two strokes. Watch the COVO video and check tooling selection inputs.
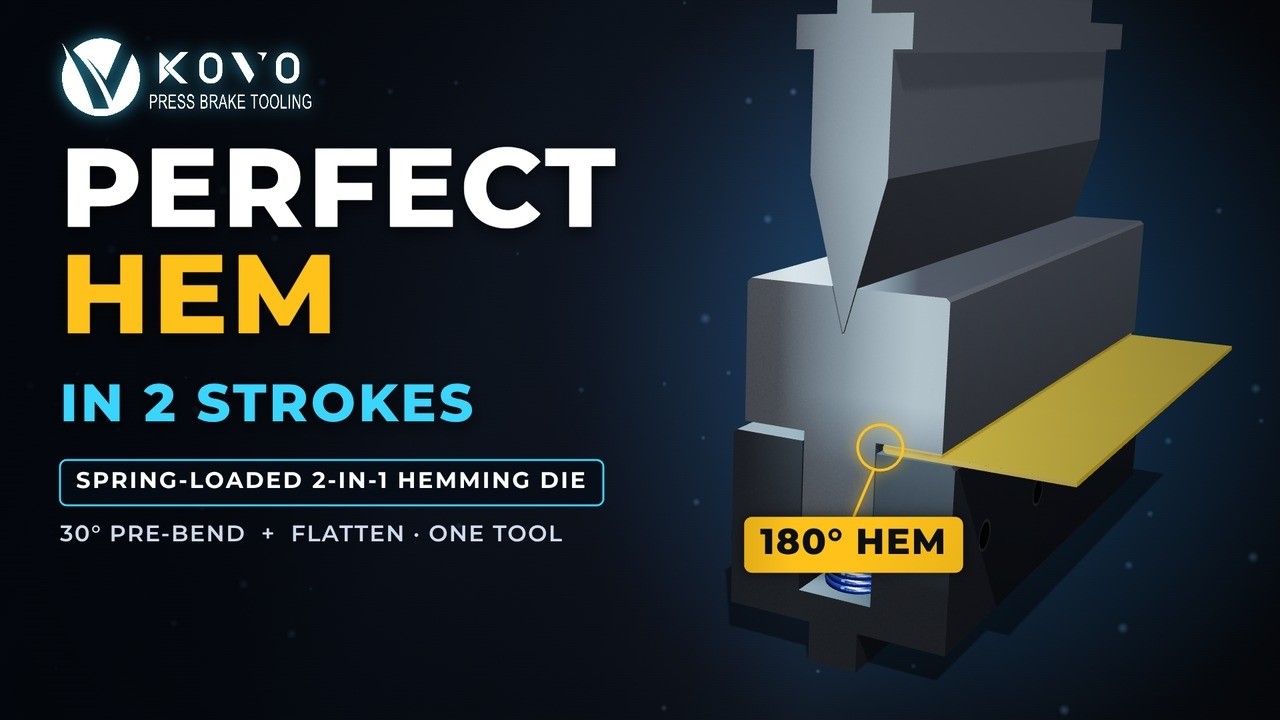
A spring-loaded hemming die combines an acute V-groove for pre-bending with a moving section for flattening the folded edge. In the COVO Precision Tooling video, the press brake makes a 30° pre-bend, the workpiece moves into the closing gap, and a second stroke produces a closed hem. The same tooling remains installed throughout the sequence. This guide explains the moving head, the two forming positions and the information needed to select a suitable arrangement. Use the animation to understand the mechanism, then review the actual material, tool drawing and load limits for your part.
How a spring-loaded hemming die works
A spring-loaded hemming die is a press brake tool that combines a pre-bending V-groove with a spring-return moving head and a closing gap. The sheet is first bent acutely, then repositioned into that gap. A subsequent ram stroke moves the head to flatten the folded edge, and the springs reopen the tool when pressure is released.
The video identifies a 30° acute punch, a 30° V-groove, a floating V-head, a flattening shoulder, a die holder and die springs. The upper groove supports the first bend. The shoulder and lower closing surface act on the prepared edge during the second operation. The spring return allows the moving section to open again for removal and the next part.
This two-position mechanism also appears in Mate's explanation of spring-loaded hemming tools, which describes acute pre-bending followed by repositioning into the closing gap. Its product specifications apply to its own tools; use COVO's approved data when reviewing a COVO arrangement.
The two strokes shown in the COVO video
- Pre-bend in the upper V-groove. The animation places the flat sheet over the top groove and brings the acute punch into the sheet. The first stroke creates the illustrated 30° pre-bend. Check support for the intended flange and the actual punch-and-die combination.
- Reposition the workpiece for closure. With the punch withdrawn, the prepared edge moves from the upper groove into the gap below the floating head. The workpiece orientation and closing position change, even though the tooling stays installed.
- Flatten in the second stroke. The punch pushes the floating head down, bringing the closing surfaces together around the folded edge. The animation then shows the closed hem and the tool reopening. Inspect the released part against the required section and surface condition.
The process saves a tool change between these two operations when the selected arrangement is suitable. It still requires a second stroke and a handling step. The video provides no measured cycle-time comparison, so it should not be used to assign a productivity percentage.
What the illustrated sheet thickness tells you
The drawing and finished-section graphics label the sheet as t = 2.0 mm (0.079 in). The closed-hem graphic also shows two sheet layers, labelled 2 × t. For that illustrated input, the overlapping straight region is approximately 4.0 mm (0.157 in) before considering the actual formed section. The fold nose, any retained gap and the inspection datum require their own drawing dimensions.
These labels describe the animation's example. They do not state a maximum thickness, material grade, guaranteed gap, tool hardness or flattening tonnage. Supply the actual sheet specification and loaded bend length when requesting an application review. A result on one material cannot establish suitability for a different grade or condition.
Selection checks before ordering a spring-loaded hemming die
- Define the finished hem. Mark whether the edge must close flat or retain an opening. Specify the important section dimensions and where they will be measured. Reject a proposal that leaves the finished gap or acceptance method undefined.
- Identify the sheet and visible face. Record material grade, actual thickness, condition, coating and protective film. Mark the cosmetic surface. Review cracking, distortion and contact marks on a representative sample instead of judging the rendered surface.
- Check flange support in the first stroke. Compare the required flange with the actual V-opening and acute punch geometry. The minimum flange length calculator is a preliminary geometry aid; it does not approve the closing position or complete hemming sequence.
- Obtain separate forming and flattening load data. Review the intended material, hem type and loaded length against the machine, punch, die, holder and adapter ratings. An air-bending force calculation does not approve the second stroke. Resolve missing load information before production.
- Review the installed heights and clearance. Check the clamp interface, open and closed tool heights, available daylight, moving-head travel, nearby returns, backgauge and removal path. A part must reach both forming positions and leave the tool without being forced past an obstruction.
- Agree on first-part evidence. Record the approved tool combination and setup, then inspect the released section, straightness and surface. Use the machine's prescribed guarding and part-support procedure. Keep hands outside the closing gap throughout the cycle.
Compare the tooling arrangements by the job
The comparison concerns how the operations are arranged. It is not a comparison of specific product capacities or measured production speeds.
| Arrangement | How the edge is formed | Suitable review question | Key condition to confirm |
|---|---|---|---|
| Separate acute-bending and flattening tools | Pre-bend the edge, then use a separate approved closing arrangement. | Can the existing tools handle an occasional hemming job? | Both operations have suitable geometry, support and load ratings. |
| Combined spring-loaded hemming die | Pre-bend on the upper V, reposition into the gap and flatten in the same installed tool. | Can a reviewed two-position tool remove the change between pre-bending and closing? | The moving head, closing contact, travel and part clearance suit the complete sequence. |
| Hydraulic hemming arrangement | A hydraulic mechanism controls the closing section in a dedicated arrangement. | Does the application justify reviewing a controlled closing mechanism? | Machine integration, hydraulic requirements and the supplier's application data are available. |
WILA's hemming guidance describes several closing arrangements and directs users to flattening load data. It also highlights surface and protective-film marking. Those general process considerations belong in the review; another supplier's thickness limits are not ratings for the COVO tool shown here.
Failure modes to inspect on the first part
- The prepared edge will not sit correctly in the gap. Check the pre-bend, flange support and positioning before changing closing pressure. Stop if the sheet slips or is driven out of the closing zone.
- The hem remains open or varies along its length. Compare the released section with the drawing. Review material variation, tool seating and the approved closing setup. Do not assign extra tonnage without the relevant load data.
- The fold cracks or the visible face is damaged. Inspect the fold nose and contact surfaces on the actual material. Record the material condition, grain direction where relevant, coating and film so the next review addresses the observed defect.
- The part collides or becomes difficult to remove. Check existing returns in both forming positions and through withdrawal. Revise the tool or sequence if clearance is inadequate. Reposition only under the machine's approved handling and safeguarding procedure.
When a standard arrangement is sufficient
A standard arrangement is a candidate when its documented interface, geometry, load rating and clearances match the intended part, and a representative first part meets the drawing. A special tool deserves review when a return blocks the closing position, a specific gap must be controlled, the folded edge cannot be removed, or the installed stack does not provide the required working space.
Start with the COVO flattening-tools family. For the broader distinction between closed and teardrop edges, read the press brake hemming tools guide. This article focuses on the spring-return mechanism and its two forming positions.
COVO Precision Tooling is the tooling brand of Nanjing Kovo Intelligent Equipment Co., Ltd., based in Nanjing, China. It manufactures standard and custom press brake punches and dies, including tooling compatible with AMADA-style, TRUMPF-style, WILA-style, LVD-style and BYSTRONIC-style systems. Confirm the actual machine interface for the selected arrangement.
FAQ
Does a spring-loaded hemming die finish the edge in one stroke?
The COVO demonstration uses two press brake strokes. The first produces a 30° acute pre-bend in the upper V-groove. The workpiece is then repositioned into the closing gap for the second stroke. The benefit shown is keeping the same tooling installed between operations, rather than completing both operations in a single stroke.
What do the springs do in a spring-loaded hemming die?
The springs return the moving head and reopen the closing gap after the ram releases it. In the demonstration, the punch drives the floating head downward during flattening. Select the complete tool from its approved drawing and load data; the presence of springs does not establish the allowable material thickness or flattening force.
Can I use the video's 2.0 mm sheet value as a capacity rating?
No. The video labels an illustrative sheet thickness of 2.0 mm (0.079 in). It does not provide the material grade, loaded bend length, machine capacity or approved tooling load. Request the rating for the actual material, thickness and hem geometry before treating a tool as suitable for that application.
How short can the hem flange be?
The flange must remain supported during the acute pre-bend and fit the subsequent closing position. The minimum depends on the actual V-opening, punch geometry, material and part profile. A minimum-flange calculator can support an initial review, but the selected hemming tool drawing and a representative first part must confirm the complete sequence.
Can the same tool produce an open or teardrop hem?
The video demonstrates a closed hem. An open or teardrop hem adds a specified opening and fold shape that must be maintained during closure. Define those dimensions and inspection locations on the drawing. Have the tooling supplier review the pre-bend radius and closing geometry before assuming that a closed-hem arrangement can produce the required opening.
Will a spring-loaded hemming die produce a mark-free surface?
Do not assume a mark-free result from the animation. Flattening creates contact on the folded edge, and the actual sheet finish or protective film can be damaged. Identify the visible face and inspect a representative sample of the intended material. Agree on the acceptable surface condition before releasing the job for production.
Next step
Request a COVO tooling recommendation with the machine model and clamping interface, material grade, thickness, bend length, finished profile, required angle or radius, quantity and visible-surface requirement. Add the hem type, any specified opening and nearby returns so the engineer can review both strokes and the removal path.
Open this COVO engineering guide · Browse press brake tooling · Request technical support