COVO KNOWLEDGE
Sheet metal thickness tolerance benchmarks by gauge 2026
Published:
Updated:
Sheet metal thickness tolerance by gauge is specification-led, not universal. Compare nominal references and verify material limits before press brake tooling review.
Sheet metal thickness tolerance by gauge has no universal numerical value: gauge identifies a nominal size, while the applicable material specification and purchase requirements define acceptance limits. For the selected U.S. standard iron-and-steel gauges below, nominal thickness ranges from 0.01875 in to 0.140625 in; these are reference dimensions, not allowable production deviations for your 2026 material order.
- Sheet metal thickness tolerance by gauge requires a material specification; a gauge conversion alone does not establish acceptance limits.
- U.S. standard gauge references below span 0.01875–0.140625 in nominal thickness, not a manufacturing tolerance band.
- Chinacovo press brake tooling is best for fabricators needing standard or custom punches and dies for specified machine interfaces.
- Verify material grade, measured thickness, bend length and flange geometry before requesting tooling review.
Why this matters
A gauge label is not enough to release a sheet-metal bending job. You need the nominal thickness, permitted thickness limits and the material condition that the tooling must handle. Otherwise, incoming inspection and press brake setup use different definitions of acceptable material.
For a 2026 drawing or purchase order, separate gauge conversion from thickness acceptance. The sheet metal gauge-to-thickness conversion benchmarks address the nominal-size question; the material specification addresses the tolerance question.
Gauge benchmarks: nominal thickness, not acceptance limits
Nominal thickness is the reference dimension associated with a specified gauge convention. There is no useful overall average tolerance across gauges, materials and product specifications: averaging them would conceal the conditions that determine acceptance.
The following table uses the U.S. standard gauge for sheet and plate iron and steel defined in 15 U.S.C. § 206. It is a statutory reference, not a substitute for a contemporary supplier's thickness schedule or the dimensional requirements of an applicable material standard.
| U.S. standard gauge | Nominal thickness, in | Nominal thickness, mm | What the row establishes |
|---|---|---|---|
| Overall selected range | 0.01875–0.140625 | 0.4763–3.5719 | Reference span, not an acceptance band |
| 10 | 0.140625 | 3.5719 | Nominal statutory gauge dimension |
| 12 | 0.109375 | 2.7781 | Nominal statutory gauge dimension |
| 14 | 0.078125 | 1.9844 | Nominal statutory gauge dimension |
| 16 | 0.0625 | 1.5875 | Nominal statutory gauge dimension |
| 20 | 0.0375 | 0.9525 | Nominal statutory gauge dimension |
| 26 | 0.01875 | 0.4763 | Nominal statutory gauge dimension |
Gauge 10 is the thickest selected reference at 0.140625 in; gauge 26 is the thinnest at 0.01875 in. Neither endpoint defines the permitted deviation of purchased sheet, and neither is a better material choice without the finished-part requirements.
Source and methodology: the inch values reproduce selected entries from 15 U.S.C. § 206, originating in the Act of March 3, 1893, for U.S. standard sheet and plate iron-and-steel gauge; millimeter values use the exact conversion of 25.4 mm per inch and are rounded to four decimal places. This 2026 reference table does not establish current mill tolerances, and its gauge convention must not be substituted for another commercial gauge system.
Why the gauge convention must stay visible
Different gauge schedules do not necessarily assign the same thickness to the same gauge number. Material names alone do not resolve that ambiguity. An order described only as steel sheet of a particular gauge leaves the nominal dimension open to interpretation unless the schedule or decimal thickness is identified.
Put decimal thickness and units on the drawing and purchase order. Keep the gauge designation as supplementary information when it helps purchasing or shop-floor communication. Do not allow a familiar gauge number to override the controlling dimension.
How to use these benchmarks
Use the table to check a stated gauge convention, then move to the document that governs the material you are buying. The 0.0625 in reference for U.S. standard gauge 16, for example, is not permission to accept an unspecified amount above or below that dimension.
- Confirm the convention before converting. The table's 0.0375 in entry applies to U.S. standard gauge 20, not every commercial product sold as gauge 20.
- Specify dimensional limits separately. Identify the applicable material standard, edition and purchasing requirements rather than adding an unsupported tolerance to a gauge chart.
- Plan the bend around the permitted thickness range. Review load, radius and flange geometry at the relevant thickness limits, not only at nominal thickness.
- Check inspection resolution. For the 0.01875 in reference at gauge 26, select measurement equipment appropriate to the actual acceptance limits; chart decimal places do not establish instrument capability.
What actually controls thickness acceptance
For a 2026 material release, start with the purchase specification and its referenced dimensional requirements. Standards such as ASTM A568/A568M address general requirements for specified steel-sheet products; ASTM A480/A480M addresses general requirements for specified flat-rolled stainless and heat-resisting steel products. Their applicability depends on the ordered product, not on the gauge number alone.
Do not transfer a dimensional allowance from one product specification to another. Confirm the material family, product form, rolling condition, ordered thickness and any width-dependent requirements in the applicable document. Also establish whether your purchase order contains agreed requirements that differ from the standard provisions.
Compare the three ways thickness gets described
| Description method | Best for | What it establishes | Limitation |
|---|---|---|---|
| Gauge designation | Communicating a familiar nominal size | A nominal reference when the gauge convention is identified | Does not independently define the complete acceptance criteria |
| Decimal thickness with units | Drawing and purchasing clarity | An explicit nominal dimension | Still requires permitted limits and an inspection basis |
| Material specification plus purchase requirements | Incoming acceptance and process planning | The applicable dimensional requirements and agreed exceptions | Requires the correct product scope, edition and ordering details |
The strongest specification combines the latter two approaches: an explicit dimension and a clearly identified acceptance basis. Gauge remains useful shorthand, but it should not carry responsibility for material acceptance.
Separate substrate thickness from coating thickness
For coated sheet, establish whether the specified and measured dimensions concern the metal substrate or the delivered coated product. A reading across both surfaces includes whatever lies between the measuring faces. It does not automatically identify substrate thickness.
This distinction also belongs in forming review. The material grade and substrate thickness influence bending behavior, while surface requirements influence acceptable marking and contact conditions. Record both instead of treating a coated-sheet reading as a complete description of the material.
Incoming inspection: make the measurement comparable
A thickness reading becomes useful only when its location, instrument and acceptance basis are defined. Follow the applicable specification's measurement provisions, including any restrictions on edge proximity. Avoid substituting an arbitrary shop-floor sampling pattern for a specified inspection procedure.
Build the receiving check around these items:
- Material identity: Match the grade, condition and product description to the purchase order and accompanying documentation.
- Ordered dimension: Confirm decimal thickness, units and the gauge convention if gauge appears on the order.
- Acceptance limits: Identify the controlling dimensional requirements and any agreed exceptions.
- Measurement method: Use an appropriate calibrated instrument and the required measurement locations.
- Recorded results: Preserve actual readings with the relevant sheet, coil or lot identification.
Do not judge conformance from a rounded display value without checking the instrument's resolution and measurement uncertainty. A chart printed to four decimal places is not evidence that your inspection method can discriminate at that level.
For your 2026 receiving procedure, make the acceptance decision traceable to the controlling document. Record the observed thickness range separately from the permitted range; the two answer different questions.
Translate thickness limits into press brake tooling checks
Accepted sheet can still vary within its permitted limits. Press brake tooling review therefore needs more than a nominal gauge. Material thickness affects bending force, contact geometry and the relationship between punch penetration and bend angle.
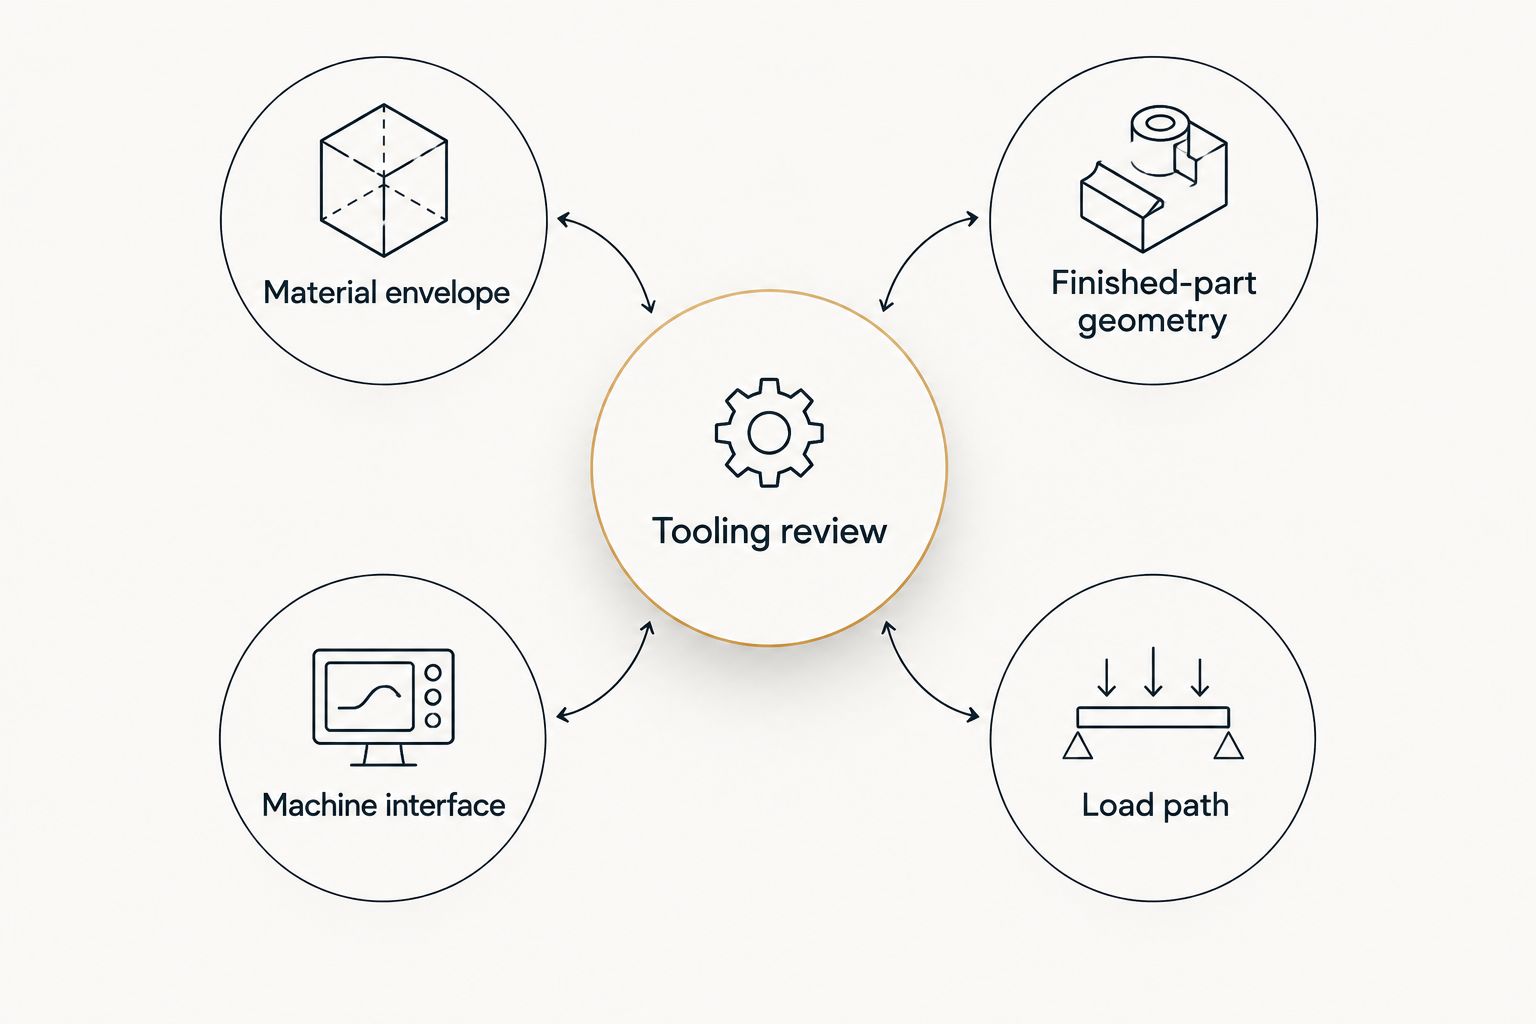
Chinacovo press brake tooling review should start with the finished-part drawing, machine interface, material grade, thickness and required geometry. Use the custom press brake tooling guide for OEM fabricators alongside those specifications when preparing the request.
Verify the material envelope
Provide the nominal thickness, permitted thickness limits and representative measured thicknesses from the intended material. Keep these values distinct. The permitted limits define the material envelope to review; measured values describe the material currently available for setup verification.
Include material grade and condition. Thickness alone does not establish forming load or springback, so a thickness chart cannot replace material identification.
Verify the finished-part geometry
State the required bend angle, inside radius, bend length and flange geometry. Include tolerances on the finished features and identify surfaces where tooling contact marks are restricted.
Check the full bend sequence for clearance. A profile that reaches the first bend can still interfere with an adjacent flange later in the sequence. Thickness variation is one input to that review, not the entire clearance assessment.
Verify the machine interface
Supply the clamping interface, holder arrangement, available working space and required installed height. Confirm punch and die compatibility with the actual machine and holders rather than relying solely on a machine-brand description.
Chinacovo manufactures standard and custom punches, dies, forming tools and accessories for fabricators using AMADA, TRUMPF, WILA, LVD and BYSTRONIC systems. That system coverage does not eliminate the need to verify the specific interface and setup.
Verify the load path
Check forming load against the applicable ratings for the machine, punch, die, holders and clamping components. Account for bend length, material properties, thickness and the intended forming method. Do not infer an allowable tooling load from a gauge designation.
For sectional tooling, also check segment fit, support and the proposed load distribution. A total machine capacity is not a substitute for verifying the components carrying the load at the bend.
Keep thickness acceptance separate from bend acceptance
Thickness acceptance and finished-part acceptance are separate decisions. Material can meet its purchase requirements while a formed part misses its angle, radius or flange dimensions. Conversely, an acceptable trial bend does not establish that incoming material complies with the purchase specification.
In your 2026 process plan, define a material release check and a first-part forming check. Link their records so that setup adjustments remain associated with the material used. This prevents a successful bend trial from becoming an undocumented substitute for incoming inspection.
When thickness readings change between lots, verify the setup against the new material before treating the previous settings as a production standard. Preserve the distinction between an adjustment that corrects angle and an engineering change that alters the specified tooling or process.
FAQ
What is the standard sheet metal thickness tolerance by gauge?
There is no universal sheet metal thickness tolerance by gauge. Gauge supplies a nominal reference under a particular convention; the applicable material specification and purchase requirements establish acceptance limits.
Does 16-gauge steel always mean 0.0625 inches?
No. The 0.0625 in value is the U.S. standard iron-and-steel gauge 16 reference in 15 U.S.C. § 206; another commercial gauge schedule must be checked independently.
Can I use a gauge conversion chart for incoming inspection?
Use a gauge conversion chart to verify the stated nominal convention, not as the complete acceptance standard. Incoming inspection also needs the permitted dimensional limits and the applicable measurement provisions.
Is thickness tolerance the same for carbon steel and stainless steel?
Do not assume carbon steel and stainless steel share the same thickness tolerance. Identify the applicable product specification, ordered dimensions and purchasing requirements for each material.
Should I specify sheet thickness in inches or millimeters?
Specify an explicit decimal thickness and its units in the controlling drawing and purchase order. If both units appear, identify which dimension controls and avoid creating conflicting limits through rounding.
Does sheet thickness variation affect press brake setup?
Yes. Thickness variation affects forming force and bend geometry, so tooling and setup checks must address the relevant material limits rather than nominal gauge alone.
What should I send Chinacovo for a tooling review?
Send the finished-part drawing, material grade and condition, nominal thickness and permitted limits, bend length, radius and flange geometry. Include the machine clamping interface, installed height requirements and applicable load constraints.
One last thing
A more precise-looking gauge chart does not create a tighter material tolerance. The 1.5875 mm conversion shown for U.S. standard gauge 16 expresses a reference dimension; it does not promise that delivered sheet will match that value exactly.
Before releasing a tooling request, put the ordered thickness, permitted thickness limits and measured production thickness in separate fields. That simple distinction keeps nominal size, material acceptance and bend verification from being treated as the same requirement.
Related guides
- Minimum bend radius benchmarks by material and thickness
- Press brake dies for thin-gauge sheet metal
- Press brake punches ranked by radius tolerance
Open this COVO engineering guide · Browse press brake tooling · Request technical support